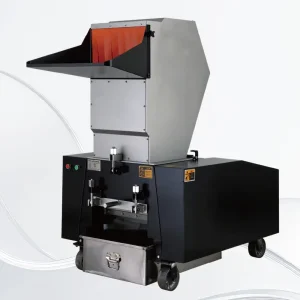
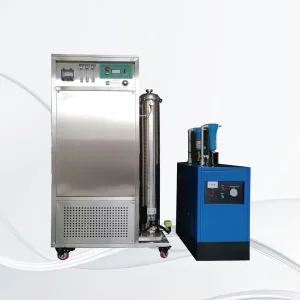
High-precision rotational molding production machinery engineered by Ningbo StarWay Roto and Orex technology engineering divisions, featuring energy-efficient heating cycles, high load-bearing carousels, and PLC smart automation.






The international polymer manufacturing landscape is undergoing a structural transformation. Global enterprise procurement is rapidly shifting from energy-intensive, internal-stress-prone methods such as heavy injection moulding and twin-sheet thermoforming toward advanced rotational moulding (rotomoulding). For large, hollow, highly durable structures—such as multi-layer chemical storage vessels, diesel DEF fuel systems, heavy vehicle hydraulic reservoirs, and insulated cold-chain containers—rotational moulding provides an unmatchable strength-to-weight ratio combined with zero internal residual mechanical stresses.
Within this industrial expansion, OEM Orex Rotomoulding Company & Service frameworks, integrated with Ningbo StarWay Roto’s manufacturing platforms, have emerged as the gold standard for tier-1 original equipment manufacturers. Originating from Jinlei Rotomolding Co., Ltd. (founded 2009) and expanding through Changzhou Yuanhuai and Taizhou OE Technology Co., Ltd. (Orex technological division), this specialized industrial collective has delivered more than 230 large-scale installations across 40+ countries. Backed by 23 proprietary invention patents, including the landmark S2-8500 mega-scale rotational moulding machine—recognized internationally as one of the largest production machines in commercial operation—the group bridges the gap between cost-effective Chinese production scalability and European precision engineering.
Official accreditation by the Ministry of Science and Technology, reflecting vertical engineering integration across finite element structural design (FEA), high-precision CNC tool cutting, and thermodynamic oven thermal airflow balancing.
How StarWay Roto and Orex technology leverage China's world-leading coastal supply chains to reduce project lead times by 45% and equipment CAPEX by 35% without compromising international performance standards.
Operating across a modern 20-acre dedicated manufacturing facility in Ningbo and Taizhou, StarWay Roto houses complete raw material pulverizing research labs, heavy structural welding bays, large 5-axis CNC portal machining centers for mould fabrication, and dedicated oven test-benches under one roof. By eliminating subcontracting delays, tool-to-machine integration tolerances are maintained within ±0.05 mm.
Over 40 specialized R&D mechanical and automation engineers form the technical foundation of our OEM division. With more than 80% holding formal mechanical engineering degrees and boasting 10+ years of rotomoulding specialization, our teams execute advanced thermodynamic simulations (CFD) to analyze heat transfer within mould chambers, ensuring uniform wall thickness and zero warpage.
Western equipment manufacturers charge substantial premiums for custom mouldings and specialized rock-and-roll configurations. Ningbo StarWay Roto provides transparent pricing matrices, rapid prototyping turnaround (from CAD to physical aluminium mould testing within 28 days), and turnkey machine-mould synchronization that slashes factory startup times by several months.
Engineered to endure severe mechanical stress, environmental weathering, chemical corrosiveness, and heavy temperature fluctuations across vital global industries.
Custom OEM manufacturing of chemical storage tanks up to 50,000L, Intermediate Bulk Containers (IBCs), acid-leach tanks, and wastewater dosing chambers. Fabricated with virgin high-density cross-linked polyethylene (XLPE) or fluoropolymer liners to prevent stress-cracking against aggressive acids and caustic agents.
Production lines for seamless diesel fuel tanks, Selective Catalytic Reduction (SCR) AdBlue/DEF reservoirs, hydraulic oil tanks, engine air-intake snorkels, and heavy tractor cabin roofs. Complies with international vehicle evaporative emission standards and impact crash-test regulations.
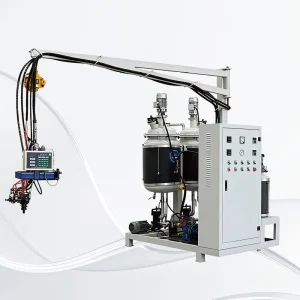
Manufacture of offshore aquaculture fish-farming cages, navigation marker buoys, marina dock pontoons, jet-ski platforms, and heavy-duty oceanographic flotation shells filled with polyurethane foam via StarWay proprietary automated high-pressure PU foaming machinery.
Double-walled, airtight roto-molded cooler boxes, dry ice shipping cases, and WHO-standard vaccine refrigeration boxes. Designed with seamless silicone gasket grooves, stainless steel latches, and high-density closed-cell polyurethane thermal cores to guarantee 7+ days of cold retention.
Automated livestock waterers, calf hutches, corrosion-proof chemical spray tanks for agricultural drones and tractors, feed hoppers, and grain chutes. Constructed from FDA food-grade, UV8-UV20 stabilized polyethylene compounds resistant to animal impact and severe outdoor sunlight.
Underground septic tanks, smart sewage inspection chambers, oil-water interceptors, spill containment pallets, and heavy refuse carts. Engineered for structural hoop stiffness under deep soil burial without hydraulic collapse or chemical permeation into municipal groundwater.
Examining the breakthrough engineering evolutions in electric heating chambers, internal mold temperature telemetry, and Industry 4.0 process analytics.
Traditional rotational moulding relied heavily on gas burners, open flames, or crude diesel heat exchangers that suffered from localized hot spots, high carbon emissions, and variable thermal currents. StarWay Roto and Orex technology pioneer closed-loop Electric Heating Rotomolding Machines. Utilizing high-efficiency ceramic infrared heating arrays, these machines reduce energy consumption per kilogram by 28%, achieve zero on-site emissions, and feature digital PID zone controls maintaining oven interior chamber uniformity within ±2°C.
The greatest variable in rotomoulding quality has historically been operator guesswork regarding cooking completion. Our modern automated shuttle and carousel units integrate wireless Peak Internal Air Temperature (PIAT) telemetry sensors directly into the core mould cavity. By measuring internal mould air temperature in real time, the PLC controller precisely detects the polymer powder lay-down, melt-flow fusion point, and cure peak, preventing under-curing (brittle parts) or over-curing (thermal degradation).
| Performance Characteristic | Legacy Open-Flame / Gas Systems | StarWay / Orex Electric & Smart Systems | Industrial Value Proposition |
|---|---|---|---|
| Thermal Chamber Uniformity | ±12°C to ±18°C (prone to hot spots) | ±2°C (Dynamic Multi-Zone PID Control) | Eliminates wall thickness variance and product warpage |
| Energy Efficiency per Cycle | High heat dissipation; 38-42% thermal loss | Direct radiation & insulated recirculating airflow (85%+ efficiency) | Saves $25,000 - $60,000 annually in plant energy overhead |
| Environmental & Workplace Safety | Combustion exhaust, CO2 emissions, fire hazard | 100% Electric, Zero Exhaust, CE compliant | Qualifies for green factory tax credits and ISO 14001 certification |
| Process Telemetry Integration | Manual timer-based cycle termination | Wireless Cavity PIAT Sensors + Cloud SCADA | Automated cycle termination based on molecular cure curves |
| Mould Changeover Time | 2.5 - 4.5 hours (manual crane clamping) | 45 - 60 minutes (Quick-Release modular spiders) | Maximizes uptime in high-mix, custom-batch OEM operations |
Procurement directors and factory engineering leads must systematically evaluate four key operational pillars before signing capital equipment or custom manufacturing agreements.
Verify that the machine's rotating arms (straight arm, offset arm, or C-arm) utilize forged alloy steels with finite-element-verified structural stiffness to prevent arm deflection when carrying multi-ton cast aluminium moulds during high-temperature rotation.
Determine if your geometry demands cast aluminium tooling (best for organic forms and high-cavity items like playground toys and kayaks) or high-density forged CNC billet aluminium (essential for tight automotive tolerances, thread inserts, and flawless mirror-polished surfaces).
Leading OEM exporters should incorporate globally serviceable industrial hardware: Siemens or Schneider PLCs, SEW-Eurodrive gear reducers, Riello or Weishaupt combustion burners, and NSK heavy spherical roller bearings to guarantee worldwide parts accessibility.
Ensure your Chinese partner conducts rigorous dry-cycling and hot-mould testing before export crating. StarWay Roto provides comprehensive video telemetry inspections, full mould trial certifications, wall-thickness ultrasonic test sheets, and ISO-compliant documentation.
In-depth technical answers curated by Ningbo StarWay Roto’s chief technology officers to clarify production dynamics, mould longevity, and factory installations.
Production tooling fabricated from high-grade A356 cast aluminium or 6061-T6 CNC billet aluminium possesses an expected production lifespan exceeding 100,000 moulding cycles when properly serviced with water-based semi-permanent release agents. Steel fabrication moulds for large bulk storage tanks can operate for 15+ years under standard industrial heating conditions.
While electricity unit costs vary regionally, electric rotomoulding machines deliver an overall thermal efficiency rating of 85-90% compared to 45-55% for gas-fired ovens. Because radiant electric elements directly heat the mould shell without generating huge volumes of combustion exhaust, heat loss is minimized, making electric models significantly cheaper in regions with strict emission penalties or high natural gas tariffs.
Our equipment accommodates the complete spectrum of rotational moulding grade resins, including Linear Low-Density Polyethylene (LLDPE), High-Density Polyethylene (HDPE), Cross-linked Polyethylene (XLPE), Polypropylene (PP), Polyamide (Nylon 6, Nylon 11, Nylon 12), Polyvinyl Chloride (PVC plastisols), and newly emerging biodegradable PLA composites.
Wall thickness in rotational moulding is governed strictly by the thermodynamic heat transfer through specific zones of the mould and the biaxial rotation speed ratio (major axis vs. minor axis). By fine-tuning the planetary rotation gearing on our PLC control consoles and optimizing mould heat sinking or thermal insulation blankets, wall thickness tolerances can be held within ±5% across critical stress points.
A standard Shuttle or Rock-and-Roll machine requires 45 to 60 days from CAD sign-off to factory dry-run testing. Large multi-arm Carousels or the custom S2-8500 platform require approximately 75 to 90 days. Custom CNC mould tooling is typically manufactured in parallel within 25 to 35 days, enabling full integrated system trials before ocean shipping.
All machines come with integrated 4G/Wi-Fi industrial IoT gateways enabling our senior automation engineers to troubleshoot PLC logic, servo drives, and thermal curves remotely in real time. For on-site commissioning, we deploy dedicated technical field engineers to customer plants globally, supported by a 14-month structural warranty and lifetime hardware support.
From multi-arm square shuttle platforms to precision polymer pulverizers and high-pressure atomizers, complete your facility's rotomoulding manufacturing loop.